Machine Vision System Market to Reach USD 26.60 Billion by 2034
Machine Vision System Market Overview
The Global Machine Vision System Market is experiencing steady growth as industries increasingly adopt automation, artificial intelligence (AI), and advanced imaging technologies to improve manufacturing efficiency and product quality. Machine vision systems enable machines to capture, process, and analyze images to perform inspection, measurement, identification, verification, and positioning tasks with high accuracy. These systems help manufacturers reduce human error, improve operational consistency, and increase production speed across industrial environments.
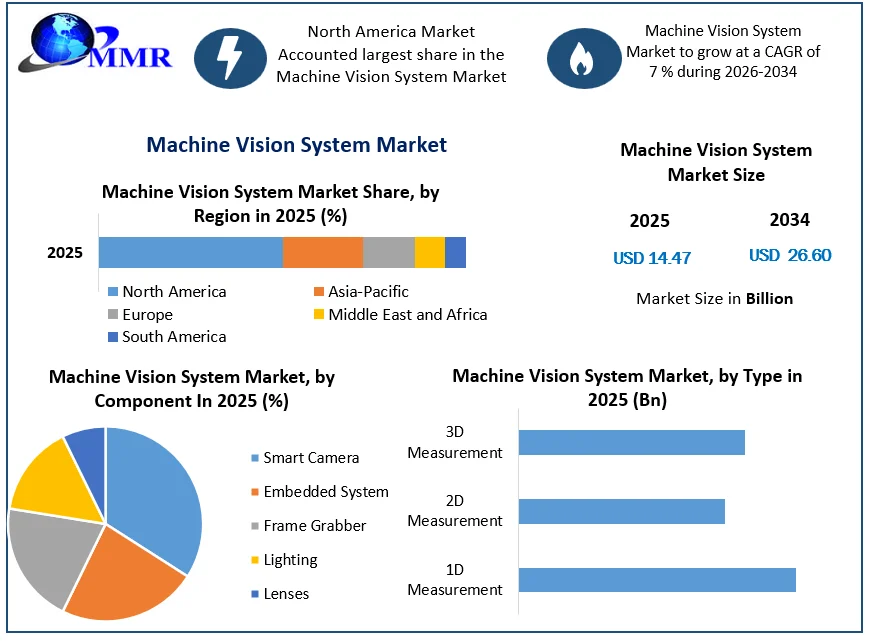
According to Maximize Market Research, the global machine vision system market was valued at approximately USD 14.47 billion in 2025 and is projected to reach USD 26.60 billion by 2034, growing at a compound annual growth rate (CAGR) of 7% during the forecast period from 2026 to 2034. Increasing investments in smart manufacturing, robotics, industrial automation, and computer vision technologies are expected to support market expansion. <Cite refs={["turn464722search0"]}/>
Machine vision technology is widely used in automotive manufacturing, electronics, pharmaceuticals, food and beverage processing, packaging, and logistics. By combining cameras, sensors, lighting equipment, lenses, and image-processing software, these systems help businesses detect defects, verify product specifications, and maintain consistent production standards.
Request for a Free Sample of This Strategic Report ➤ https://www.maximizemarketresearch.com/request-sample/55112/
Machine Vision System Market Growth Drivers
Increasing Adoption of Industrial Automation
The growing demand for industrial automation is one of the major factors driving the machine vision system market. Manufacturers are investing in automated production lines to increase output, reduce operational costs, and improve manufacturing accuracy. Traditional manual inspection methods can be time-consuming and inconsistent, particularly in high-volume manufacturing environments.
Machine vision systems support continuous inspection and provide repeatable results, enabling manufacturers to identify defects and correct production issues more quickly. Their integration with robotic systems, programmable controllers, and manufacturing execution systems also improves coordination across production facilities.
As industries move toward smart factories and connected manufacturing environments, machine vision technology is becoming an important component of modern industrial operations.
Rising Demand for Quality Inspection and Defect Detection
Product quality and safety have become important priorities for manufacturers across several industries. Machine vision systems inspect products for surface defects, dimensional variations, incorrect assembly, missing components, and packaging errors. Automated inspection helps businesses maintain consistent quality standards while reducing waste and product recalls.
In the automotive industry, machine vision is used to inspect components, verify assembly processes, measure dimensions, and guide robotic operations. Electronics manufacturers use these systems to examine printed circuit boards, semiconductor components, and miniature electronic parts that require precise inspection.
The ability to perform rapid and reliable inspections is expected to encourage broader adoption of machine vision solutions across manufacturing sectors.
Advancements in Cameras, Sensors, and AI
Continuous improvements in complementary metal-oxide-semiconductor (CMOS) sensors, smart cameras, image-processing hardware, and computer vision software are expanding the capabilities of machine vision systems. Modern solutions can capture detailed images, process visual information quickly, and identify complex defects with greater precision.
The integration of AI and deep learning is also enabling systems to recognize irregular patterns and handle inspection tasks that are difficult to manage using conventional rule-based methods. These capabilities are particularly useful when manufacturers deal with product variations, complex surfaces, and changing production conditions.
Machine Vision System Market Restraints and Challenges
High Initial Investment and Integration Costs
The high initial cost of machine vision equipment can restrict adoption, particularly among small and medium-sized enterprises. Advanced cameras, specialized lenses, lighting systems, processing hardware, and software can require substantial investment. Additional expenses may arise from system integration, employee training, maintenance, and production-line modifications.
Companies must evaluate the expected productivity improvements and long-term cost savings before implementing these systems. The availability of scalable and cost-effective solutions will be important for expanding adoption among smaller manufacturers.
Shortage of Skilled Professionals
Machine vision systems require expertise in imaging, optics, software development, industrial automation, and data analysis. A shortage of trained professionals can make implementation and troubleshooting more difficult. Inadequate training may also prevent businesses from fully utilizing the capabilities of advanced inspection technologies.
Manufacturers and technology providers can address this challenge through employee training, technical support, simplified software interfaces, and solutions that require less specialized programming.
Integration With Existing Infrastructure
Integrating machine vision equipment into older manufacturing facilities can present technical challenges. Differences in communication protocols, production equipment, software platforms, and data systems may increase implementation time and costs.
Reliable performance also depends on appropriate lighting, camera positioning, image quality, and environmental conditions. Vendors that provide flexible integration capabilities and comprehensive technical support may gain a competitive advantage.
Machine Vision System Market Segmentation Analysis
The global machine vision system market is segmented by component, type, application, industry vertical, and region. These categories help identify major demand areas and emerging investment opportunities.
By Component
The component segment includes smart cameras, embedded systems, frame grabbers, lighting, and lenses. Smart cameras are an important category because they combine image acquisition and processing capabilities within a compact device. Their relatively straightforward installation and suitability for automated inspection make them attractive for industrial applications.
Embedded systems support image processing and machine vision functions within specialized hardware environments. Frame grabbers capture image data from cameras and transfer it to processing systems, while lighting equipment and lenses help produce clear and consistent images for accurate analysis.
Continued improvements in sensor performance, processing power, and compact imaging technology are expected to support demand across component categories.
By Type
Based on type, the market includes 1D measurement, 2D measurement, and 3D measurement systems.
Two-dimensional machine vision is commonly used for surface inspection, pattern recognition, barcode reading, and product identification. One-dimensional measurement systems support applications involving linear image analysis and continuous material inspection.
Three-dimensional machine vision provides depth information and spatial measurements, making it suitable for complex dimensional inspection, object recognition, and robotic guidance. As manufacturers increasingly automate tasks involving irregular objects and precise positioning, 3D vision solutions are gaining importance.
By Application
The application segment includes positioning, identification, verification, and measurement. Identification applications involve reading barcodes, labels, serial numbers, and other product information. These capabilities help improve traceability, inventory management, and packaging accuracy.
Verification systems determine whether products, components, or labels meet specified requirements. Measurement applications evaluate dimensions and tolerances, while positioning systems provide visual guidance for robots and automated equipment.
The growing need for accurate product tracking, automated inspection, and reliable robotic operations is expected to support demand across these applications.
By Industry Vertical
The market serves industrial manufacturing, healthcare, electronics, automotive, and other industries. Automotive manufacturing represents an important application area because production processes require precise component inspection, assembly verification, and automated quality control.
The electronics industry also creates substantial demand due to the increasing complexity and miniaturization of electronic components. Machine vision systems help inspect circuit boards, connectors, and semiconductor-related products.
In healthcare and pharmaceutical manufacturing, these systems support packaging inspection, label verification, product identification, and quality assurance. Food processing and logistics applications include package inspection, sorting, product counting, and automated handling.
Request for a Free Sample of This Strategic Report ➤ https://www.maximizemarketresearch.com/request-sample/55112/
Regional Analysis of the Machine Vision System Market
Asia Pacific is a leading region in the machine vision system market, supported by its strong electronics manufacturing base, automotive production, and increasing investments in industrial automation. Countries such as China, Japan, South Korea, and India provide important opportunities for machine vision suppliers as manufacturers modernize production facilities and improve quality-control processes.
Europe represents another significant market because of its established automotive industry, advanced engineering capabilities, and emphasis on manufacturing efficiency. Germany and other industrial economies provide demand for automated inspection, precision measurement, and robotics-enabled production.
North America benefits from investments in advanced manufacturing, robotics, semiconductor production, and AI-enabled industrial technologies. Manufacturers across the United States, Canada, and Mexico are potential users of machine vision solutions for quality control and production optimization.
The Middle East and Africa and South America also offer opportunities as industrial modernization, manufacturing investments, and logistics automation expand. Market growth in these regions will depend on infrastructure development, technology accessibility, skilled labor availability, and investment in automated production systems.
Competitive Landscape and Key Players
The machine vision system market is competitive, with companies focusing on technological innovation, product development, software integration, and strategic partnerships. Market participants are developing advanced cameras, image-processing platforms, inspection software, and integrated automation solutions to address changing industrial requirements.
Major companies identified in the market include:
-
Cognex Corporation
-
Teledyne Technologies, Inc.
-
Keyence Corporation
-
National Instruments Corporation
-
Basler AG
-
Baumer Optronic GmbH
-
SICK AG
-
Omron Corporation
-
Allied Vision Technologies GmbH
-
Datalogic S.p.A.
-
Sony Corporation
-
Canon Inc.
-
Intel Corporation
-
JAI A/S
-
IDS Imaging Development Systems GmbH
-
ISRA Vision
Companies are increasingly investing in AI-enabled inspection, high-resolution imaging, 3D vision, and robotics integration to strengthen their market positions. Partnerships between machine vision providers and automation companies can also help manufacturers deploy inspection and robotic applications more efficiently.
Recent Developments in the Machine Vision System Market
Recent developments highlight the growing importance of advanced imaging and AI-driven industrial automation.
In September 2026, Cognex Corporation entered into an agreement to acquire RealSense, with the aim of expanding its capabilities in 3D robotic perception. This development reflects increasing interest in vision technologies that support robotic automation and complex industrial tasks.
In January 2026, Teledyne Judson Technologies announced the SCION family of short-wave infrared (SWIR) cameras. These cameras expand high-performance imaging options for demanding industrial and scientific applications.
In September 2025, ABB Robotics partnered with LandingAI to integrate RobotStudio with LandingLens, supporting the deployment of AI-enabled robotic applications. In June 2025, Cognex launched OneVision, an integrated machine vision software framework designed to support high-speed industrial inspection.
These developments demonstrate how manufacturers and technology providers are combining imaging hardware, AI software, and robotics to improve inspection performance and production efficiency. <Cite refs={["turn464722search0"]}/>
Future Outlook of the Machine Vision System Market
The future of the machine vision system market will be shaped by the continued adoption of smart manufacturing, AI-powered inspection, advanced imaging sensors, and autonomous robotics. Manufacturers are expected to place greater emphasis on real-time defect detection, predictive quality management, product traceability, and data-driven production optimization.
The integration of machine vision with industrial Internet of Things platforms and connected manufacturing systems may further improve visibility across production operations. More accessible software, modular equipment, and scalable solutions could also help smaller businesses adopt automated inspection technologies.
However, suppliers will need to address implementation costs, workforce training, and integration complexity to support broader market penetration. Companies that combine accurate imaging, reliable software, flexible integration, and strong technical support are likely to be well positioned to benefit from industry demand.
Conclusion
The global machine vision system market is expected to expand steadily as manufacturers increasingly prioritize automation, product quality, operational efficiency, and intelligent inspection. Valued at USD 14.47 billion in 2025, the market is projected to reach USD 26.60 billion by 2034, registering a CAGR of 7% from 2026 to 2034.
Advancements in AI, smart cameras, 3D imaging, and robotic guidance are creating new opportunities across automotive, electronics, healthcare, and industrial manufacturing. Although high investment costs and integration challenges may affect adoption, continuous technological innovation and the expansion of smart factories are expected to support long-term market growth.
About Maximize Market Research
Maximize Market Research Pvt. Ltd. (MMR) is a global market research and consulting company that provides reliable, data-focused, and practical business insights. The firm serves a wide range of industries, including healthcare, pharmaceuticals, technology, automotive, electronics, chemicals, personal care, and consumer goods. Through market forecasts, competitive analysis, strategic consulting, and industry impact assessments, MMR helps organizations understand changing market conditions, identify growth opportunities, and make informed business decisions for long-term success.
Contact US:
2nd Floor, Navale IT Park Phase 3
Pune Banglore Highway, Narhe
Pune, Maharashtra 411041, India
+91 9607365656
sales@maximizemarketresearch.com

 French